
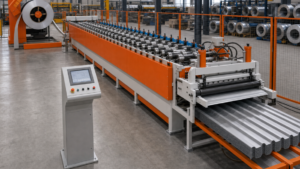
Multi-Profile Roofing Roll Former: Is It Right for Your Order Mix?
A four-profile roofing roll-forming line fits recurring, compatible panel work when the shop can group production and support the complete coil-to-cut-to-discharge flow. Dedicated equipment is usually stronger when one profile dominates, changes are frequent, or the material and geometry fall outside the documented envelope.
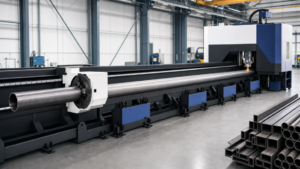
HSG TS2 V2.0 for High-Mix Tube Cutting
The HSG TS2 V2.0 is worth evaluating when short-run tube work includes holes, slots, contours, or selected bevel and weld-preparation features—not just straight cuts. This guide explains where 3D tube-laser processing can improve routing and where a saw, drill, flat-laser route, or outsourcing may still be the better fit.
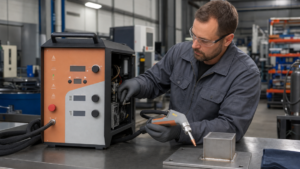
IPG LightWELD Preventive Maintenance
Consistent IPG LightWELD welding and cleaning results depend on optical care, consumable control, safety-function verification, useful records, and a clear boundary between routine maintenance and qualified service.
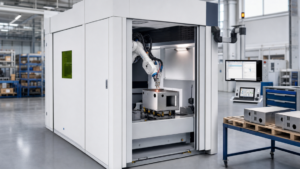
TRUMPF TruLaser Weld 3000 for High-Mix Welding
The TRUMPF TruLaser Weld 3000 is aimed at small-batch sheet-metal assemblies where compact robotic access, CAD-based programming, and repeatable fit-up can turn variable work into flexible laser-welding capacity.
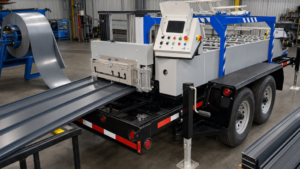
SSQ II Discontinuation: SSQ3 vs. SSQ II
The SSQ II MultiPro order window ends September 30, 2026. The SSQ3 keeps the 16-profile platform while changing tooling, controls, safety features, power options, and the practical buying decision for roofing and architectural-sheet-metal teams.
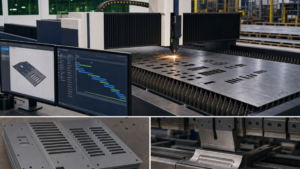
Laser-Cut Louvers and Embosses on a Press Brake
A CNC press brake with special forming tooling can produce selected louvers, embosses, clips, countersinks, and extruded holes in laser-cut blanks. The practical boundary depends on feature geometry, blank preparation, tooling, machine access, changeover, and production volume.
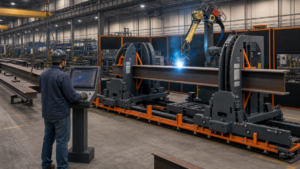
1872’s Autonomous Factory: Is Robotic Beam Welding the Next Step?
1872’s July 2026 factory announcement points toward software-orchestrated fabrication, but a focused robotic beam-welding cell is the more practical next step for shops with suitable structural-steel work, usable CAD data, and the operating discipline to support automation.
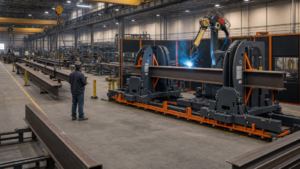
AGT BeamMaster Layout: Floor Space and Crane Access
An AGT BeamMaster cell needs more than its published machine envelope. The Light, Plus, or Twin configuration must be matched to the longest member’s handling route, crane coverage, safeguarded access, fit-up, inspection, and outfeed staging.
Fibermak Momentum Gen-5 Alarm and Cut-Quality Service Preparation
How to separate a Fibermak Momentum Gen-5 alarm from cut-quality drift, preserve the right machine and process evidence, and decide when remote support, parts coordination, or onsite service is appropriate.
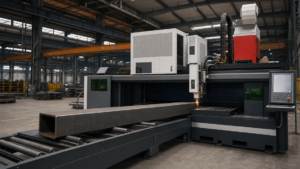
Large-Tube Laser vs. Saw-and-Drill Routing for HSS
A large-tube fiber laser can replace more than a saw when HSS and structural profiles carry holes, slots, notches, miters, or weld-preparation features. The decision depends on feature density, the validated material envelope, handling, programming, and the work that should remain on a saw, drill, or machining center.
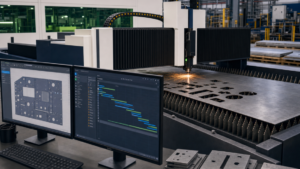
Automatic Laser Nesting: Yield vs. Production Flow
Automatic nesting for the HSG G3015H can reduce programming effort and improve material decisions, but the best production result balances utilization with cut reliability, remnant control, job priority, part identification, sorting, and downstream bending capacity.
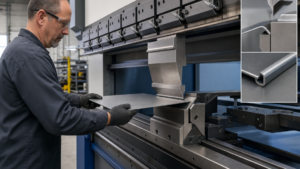
Choosing Press Brake Hemming Tooling
An existing CNC press brake can often form a closed or gapped hem without moving the part to another forming machine. The right choice among a conventional two-hit sequence, two-stage die, bend-and-hem tool, and custom gapped tooling depends on material range, flange geometry, machine compatibility, surface requirements, and recurring production volume.

HYDMECH M-20A-120 for Long-Stock Miter Cutting
The HYDMECH M-20A-120 makes sense for structural fabricators that need repeatable miter cuts, automatic indexing, and powered movement of long stock. Its value depends on the actual profile-and-angle mix, material-flow layout, optional bundle-cutting needs, and the downstream work that follows the saw.

Should Your Second Fiber Laser Match the First?
Match a second flat-sheet fiber laser when interchangeable capacity is the goal. Choose a different platform only when it solves a measured format, material, thickness, or automation constraint.
NovAI Autonomy and Robotic Welding Capital Timing
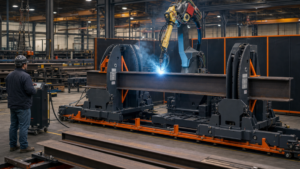
NovAI’s ABB and Yaskawa expansion changes the proof required in a robotic-welding capital review, but it does not justify delaying a needed structural-welding capacity investment.