Dave Graf
Dave Graf
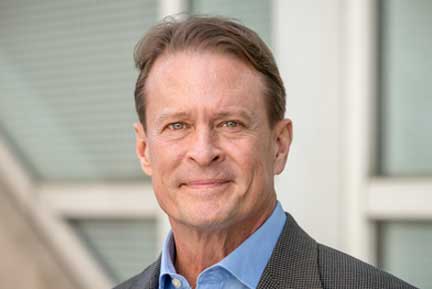
Regional Sales Executive
Before beginning a 30 plus year career in Industrial Sales and Sales Management, Dave was a professional musician for a 10 year span as a guitarist/vocalist/songwriter. He and his wife of 33 years Kathy, relocated from their hometown of Chicago in ‘97 to Scottsdale, AZ where they spend much of the year along with son Matt, daughter Kylie and wonder dogs Gracie and Rizzo (you can take the Cubs fans out of Chicago but….!)
Related Articles
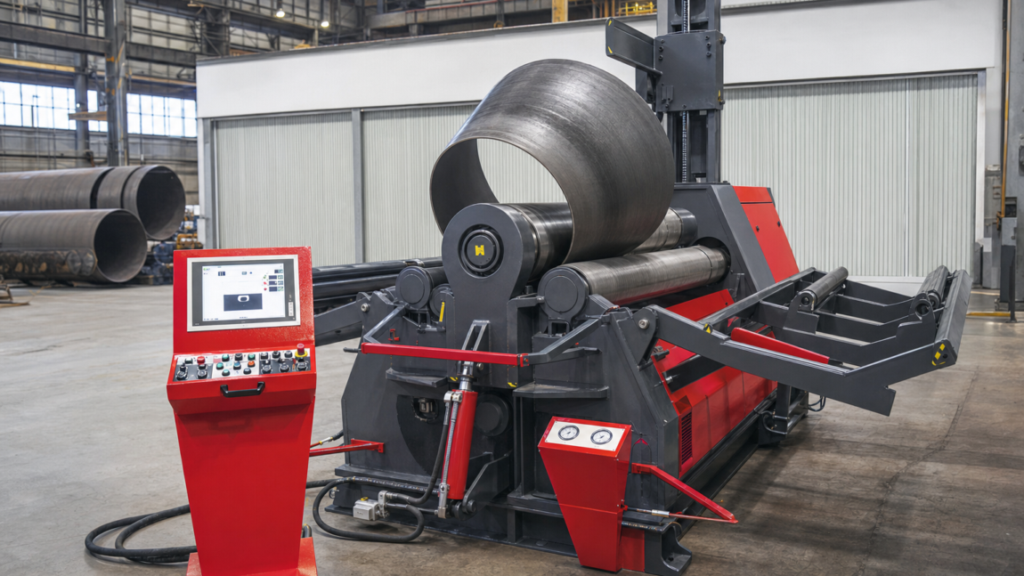
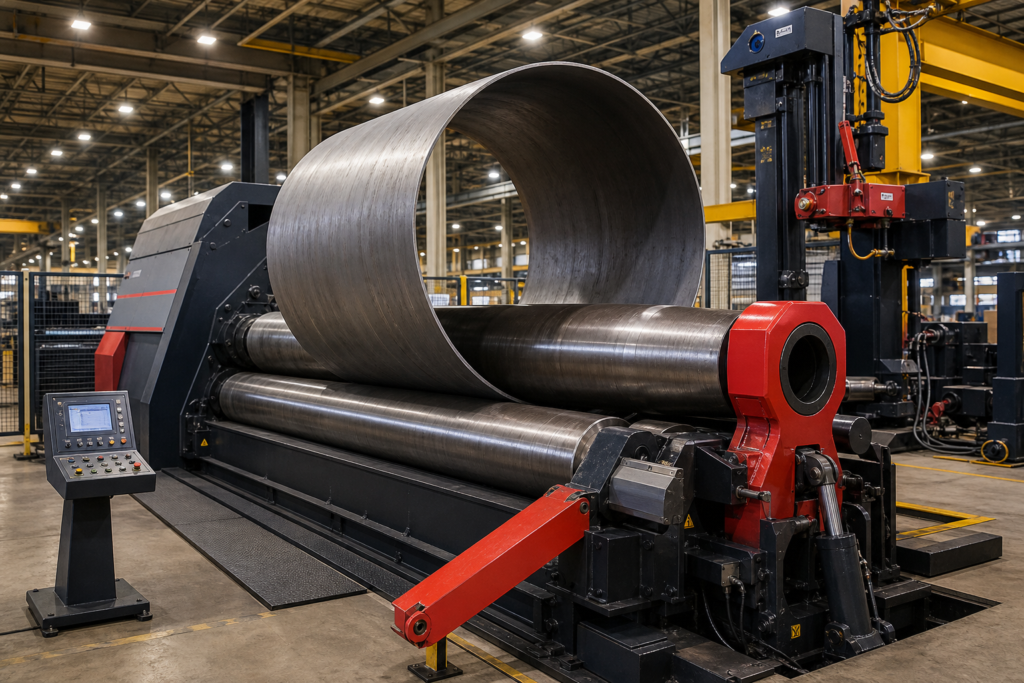
JSW Baytown Upgrade: Four-Roll Plate-Roll Capacity
JSW’s Baytown plate-mill upgrade is a reason to review four-roll plate-roll requirements, not a reason by itself to buy a larger machine. Match the decision to the plate your shop can obtain and the parts it must form.ADOP Plate Processing for Drilling and Plasma Bevel Cutting
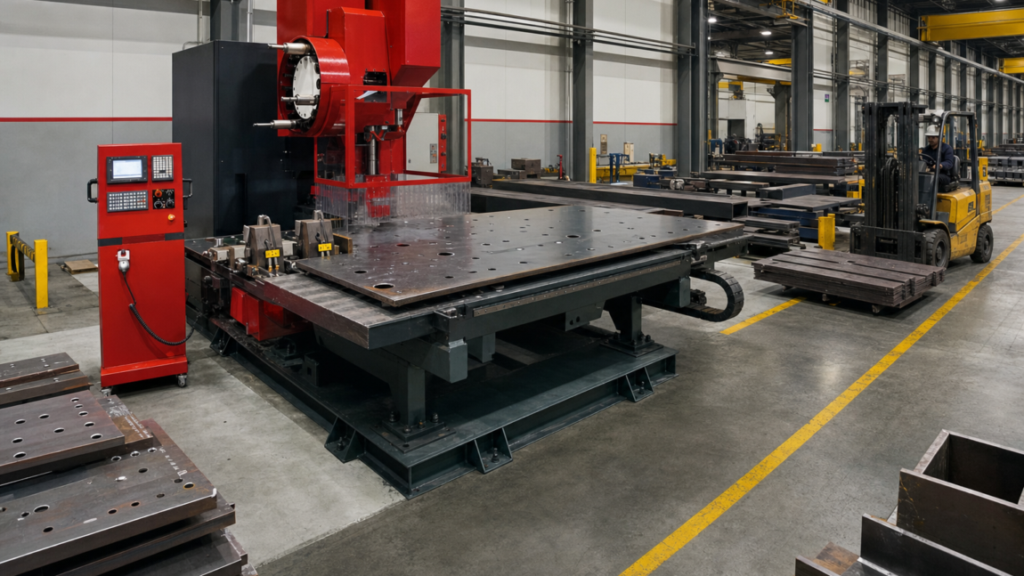
The ADOP combines CNC drilling, tapping, countersinking, marking, plasma or oxy-fuel cutting, and beveling for structural plate parts that require several operations before welding or assembly. It fits best when reducing transfers and manual weld preparation matters more than maximizing one isolated operation.AFD Plate Drilling Cell Layout for Structural Steel Shops
The AFD improves structural-plate throughput when loading, drilling, marking, tapping, outfeed, and the next operation are designed as one controlled material-flow route.IMTS 2026: Evaluate Heavy Material Handling Before More Capacity
IMTS 2026 makes material flow part of the automation conversation. For heavy fabricators, the AMTEK material-handling offering provides a concrete option to evaluate before another processing machine adds capacity to an already congested route.AISC 360 and 341 Drafts: What Structural Shops Should Review
The AISC 360 and AISC 341 drafts do not require an immediate machine change. Structural shops should review contract requirements, approved detailing data, NC1 or DSTV release, measurement, marking, and inspection controls before changing production methods.AGT BLOK Robotic Welding: Material Flow Before Arc Time
AGT BLOK can improve robotic welding productivity only when cut components, fit-up, fixtures, handling, access, and finished-part removal keep pace with the cell. The 1872 Factory One story shows why material flow should be designed before arc time becomes the headline metric.AGT BeamMaster Layout: Floor Space and Crane Access
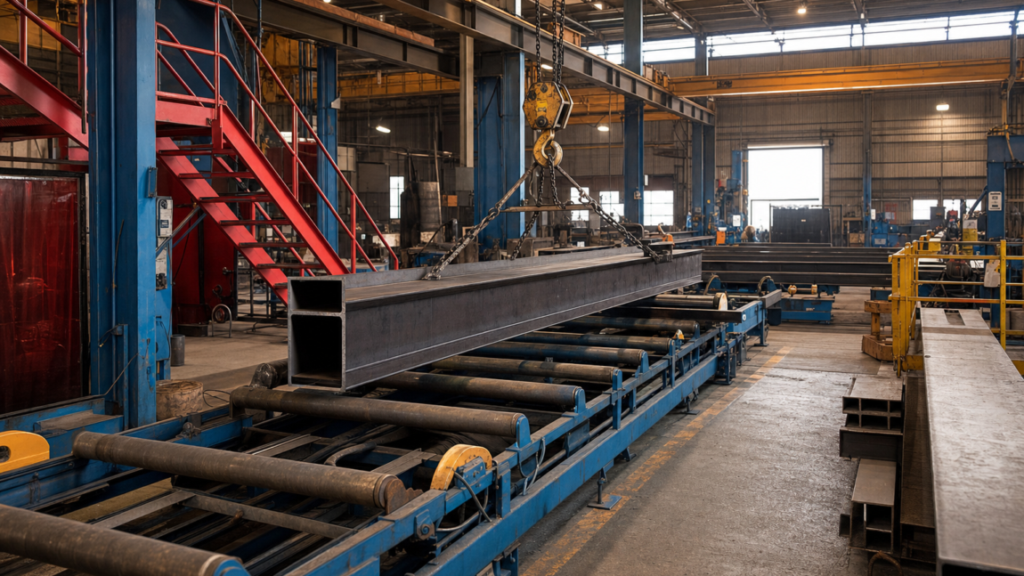
An AGT BeamMaster cell needs more than its published machine envelope. The Light, Plus, or Twin configuration must be matched to the longest member’s handling route, crane coverage, safeguarded access, fit-up, inspection, and outfeed staging.Akyapak 3 ADM VENERA for Weld-Access Beam Preparation
The Akyapak 3 ADM VENERA is worth evaluating when structural members repeatedly need multi-face drilling plus chamfering or rathole-style weld-access preparation. This guide explains when that capability changes the choice over a standard 3 ADM or 3 ADM ECO.Can AGT BeamMaster Rotators Reduce Crane Moves?
AGT BeamMaster rotators can reduce repeated crane-supported flips and repositioning during structural-steel welding when compatible pre-fit members fit the cell envelope and the shop plans the remaining load-in, load-out, service, and exception work.AGT LayoutMaster for Structural Steel Fitting
The AGT Robotics LayoutMaster projects 3D CAD fitting information onto beams, HSS, channels, angles, plates, and structural assemblies. It can reduce manual layout, but the application still depends on controlled CAD data, repeatable workpiece alignment, clear crane and operator access, and a material path that supports fitting through welding.Davi’s Expanded North American Support for Plate-Roll Buyers
Davi’s expanded North American support operation can make application testing, training, parts planning, and retrofit review more practical for 4-roll plate-roll buyers, but it does not replace machine-fit validation.AMTEK APC 1200 Beam Coping: Plasma or Oxy-Fuel?
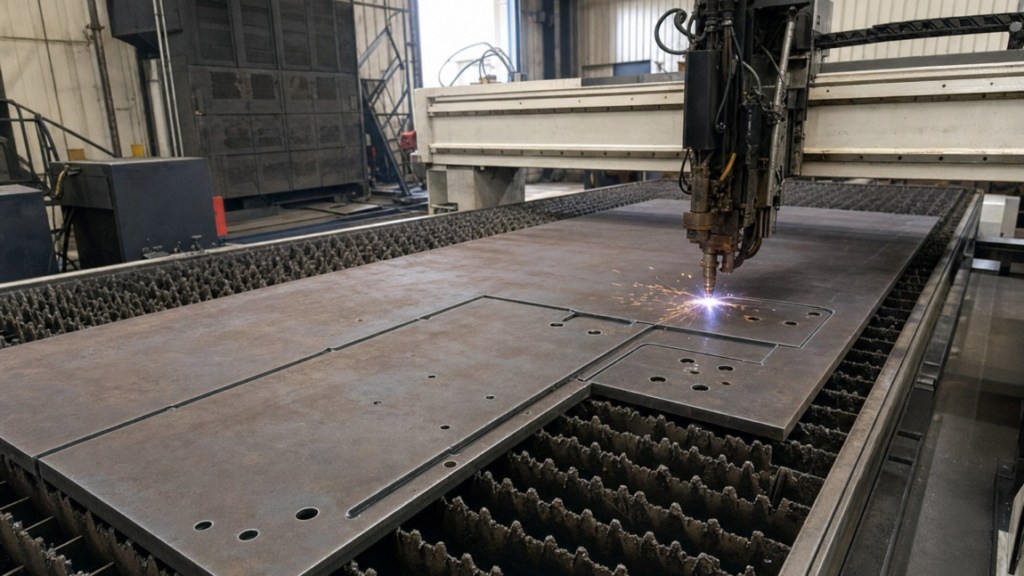
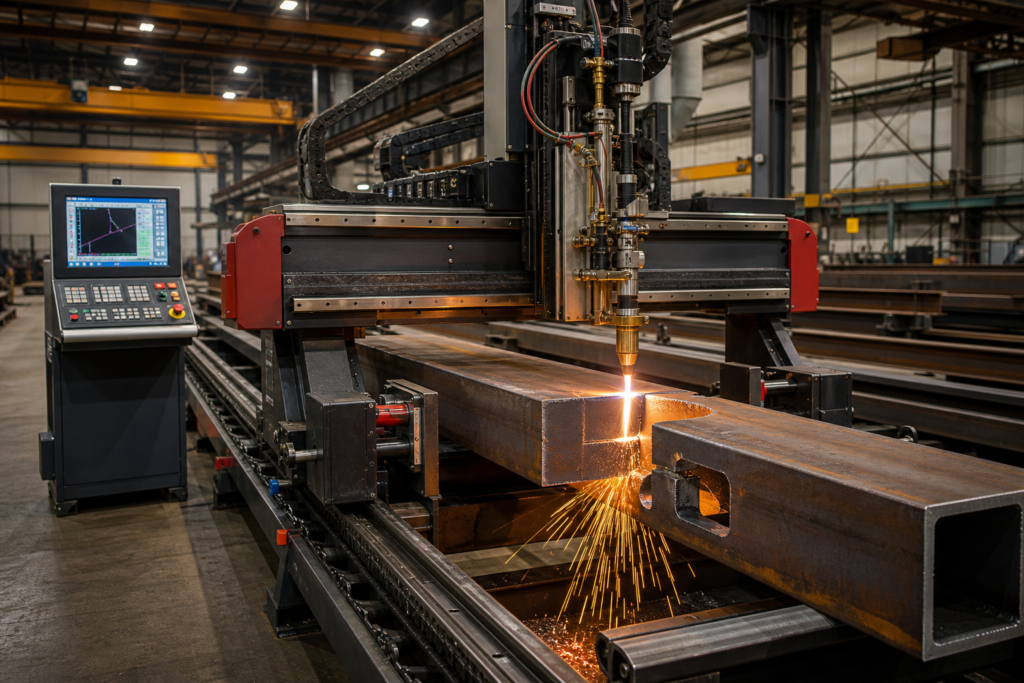
The AMTEK APC 1200 fits structural fabricators that need repeatable CNC coping, beveling, profiling, and related thermal cuts across beams and other structural profiles. Oxy-fuel remains the practical choice for thick sections and difficult access, while plasma can add throughput on thinner work only when the exact APC 1200 configuration, pierce limit, torch access, and cut-quality requirements are verified.