AMTEK Beam Rotators for Structural Steel Fabrication
Learn when recurring beam turns may justify evaluating AMTEK’s material-handling offering, and what to confirm about beam fit, layout, interfaces and rated limits.

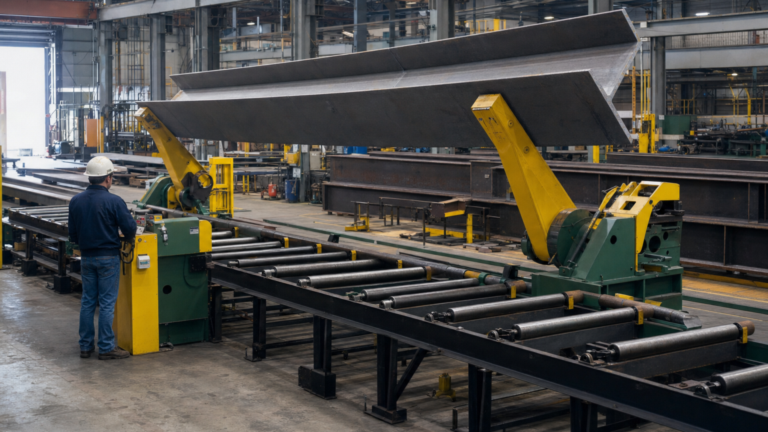
Learn when recurring beam turns may justify evaluating AMTEK’s material-handling offering, and what to confirm about beam fit, layout, interfaces and rated limits.
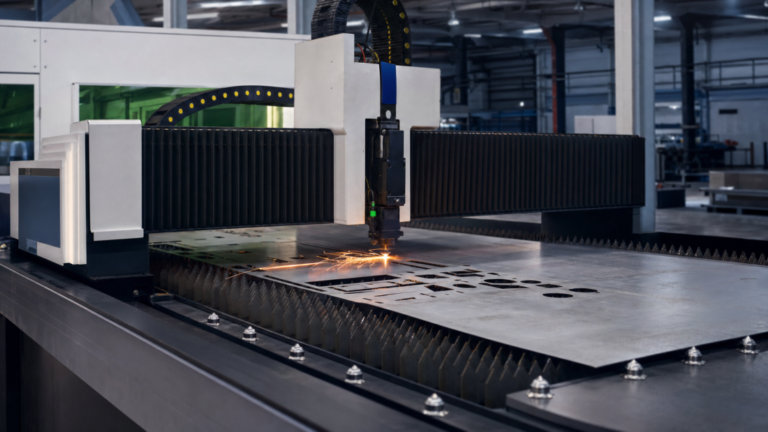
When a flat-sheet laser department is overloaded, the right investment depends on whether cutting time, available machine hours, or material handling is the constraint. Use the HSG G3015H and Store Pro 3015 as concrete options, then prove the choice with job-history and utilization data.
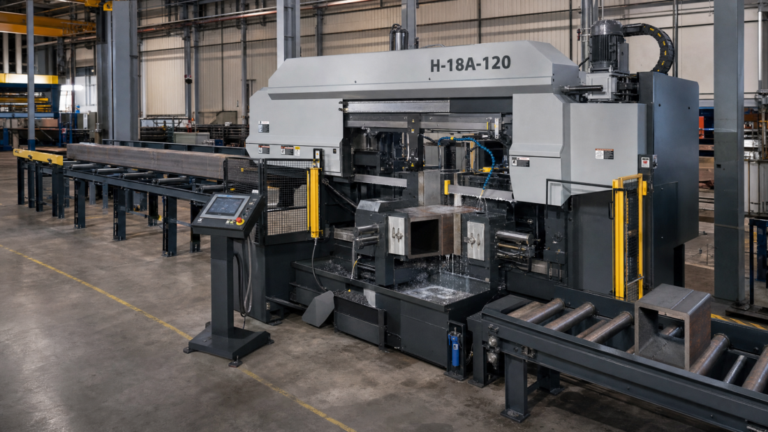
The HYDMECH H-18A-120 is a practical first modernization step when repeated 90-degree cutting, manual indexing, and long-stock handling constrain a legacy cell. Its 10-foot bar feed, automatic indexing, hydraulic clamping, split front vise, stored jobs, and handling options improve the saw operation without replacing downstream drilling, coping, fit-up, welding, coating, or shipping processes.
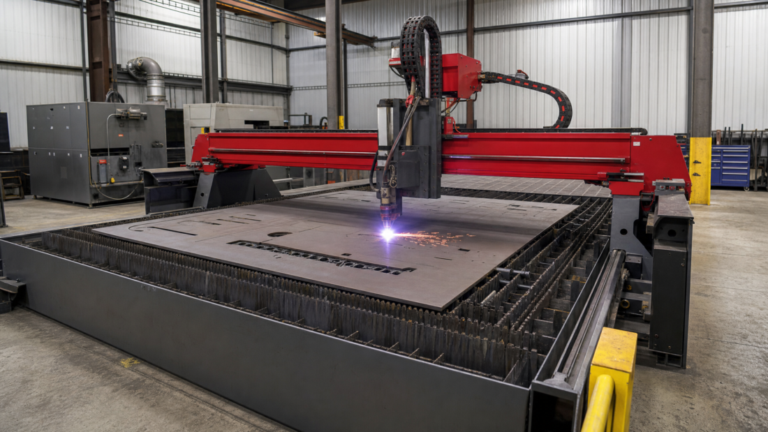
A clean plasma-cut coupon is not enough to approve a heavy-fabrication project. Representative parts should prove the proposed Akyapak cutting scope, process repeatability, material flow, downstream fit, and installation interfaces before capital approval.
A carbon-steel fabrication shop can take on stainless structural work only when its material route controls the contact points that create surface contamination and late-stage cleanup. This field guide helps plant managers choose a dedicated stainless route, controlled shared equipment, or outside finishing capacity.
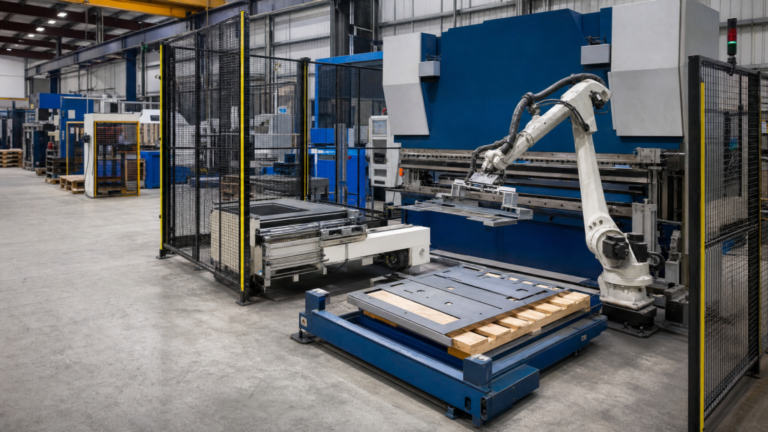
A multi-machine line is not ready for layout approval until each handoff defines part state, handling path, buffer behavior, control authority, recovery, access, and acceptance responsibility.

The strongest first bridge welding automation scope is not necessarily the weld family with the most manual arc hours. It is the component that can move through engineering, fit-up, welding, inspection, repair, records, and outbound handling without an unresolved ownership or plant-flow gap.
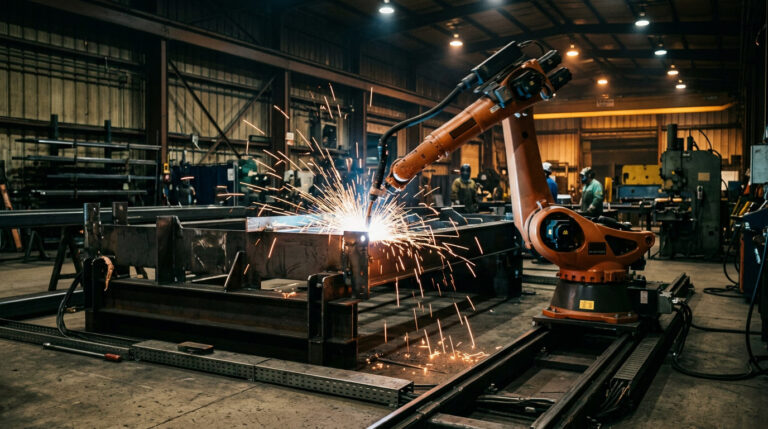
A first folder-handoff project should be defined by approved part families, orientation, support, control states, and recovery paths—not by a robot brand or headline cycle rate.
A forming line is not finished at cutoff. When stack condition, protection, counts, labels, pallet patterns, and shipping release slow finished-goods flow, define the shipping unit first and scope automation backward from there.
End of content
End of content