AGT BLOK Large-Weldment Robotic Welding
AGT BLOK fits large, variable weldments needing extended robot travel and configurable positioning. Evaluate usable welding capacity and the complete application under the revised R15.06 safety framework.

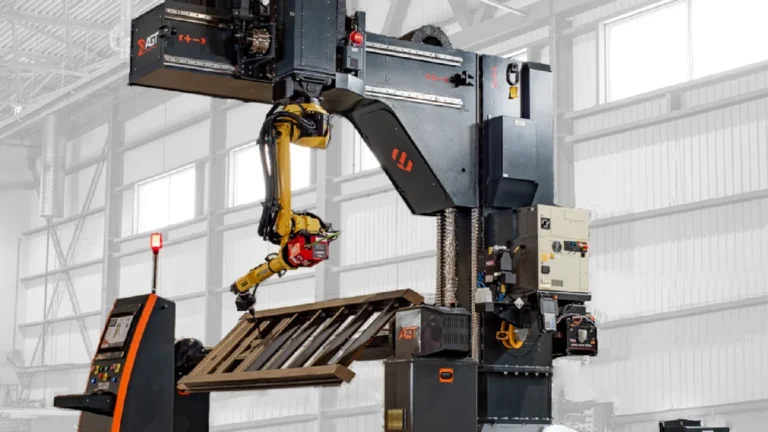
AGT BLOK fits large, variable weldments needing extended robot travel and configurable positioning. Evaluate usable welding capacity and the complete application under the revised R15.06 safety framework.
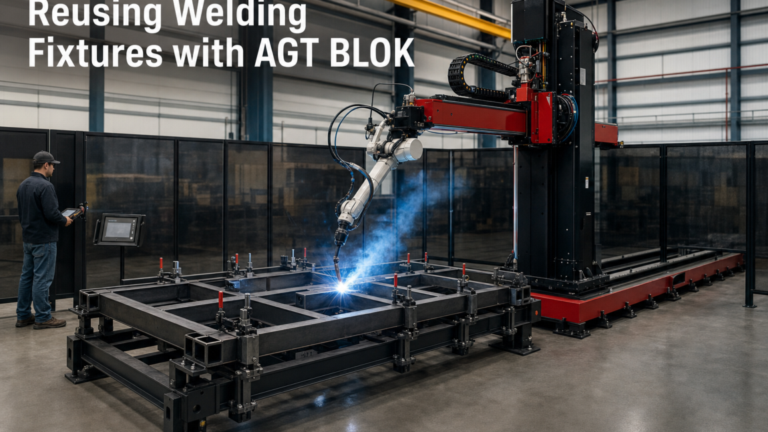
AGT BLOK supports customer-supplied tables or trestles. Evaluate whether existing welding fixtures should be retained, modified or replaced.
A SnapCam-equipped AGT BLOK can adjust a weld path to measured joint position. Fit-up, assembly stability and torch access still need separate control.
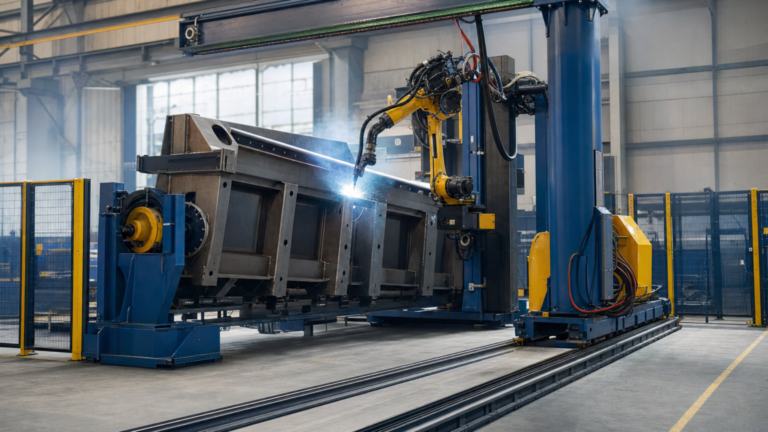
A new PEMA WeldControl workflow adapts multi-pass patterns to measured groove geometry. For high-mix buyers, that is a different capability from creating programs or correcting joint location.
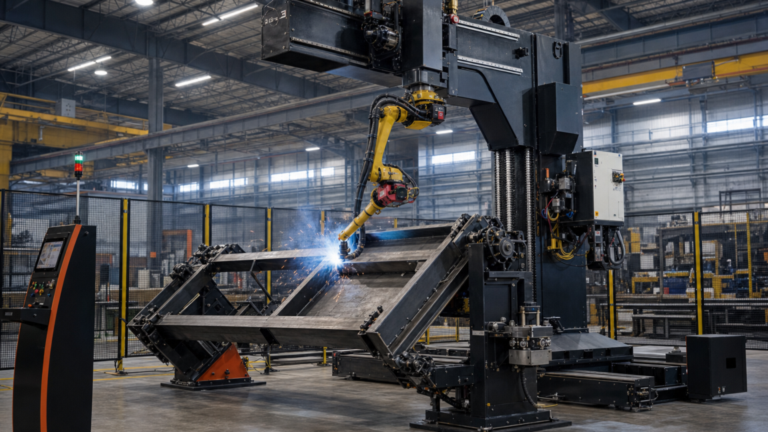
AGT BLOK is a practical candidate for fabricators that repeatedly weld medium-to-large frames, skids, trailers, trusses, containers, and other complex assemblies in changing batches. The fit depends on recurring part families, consistent presentation, useful positioning, validated programming, safeguarding, training, and clear ownership after commissioning.
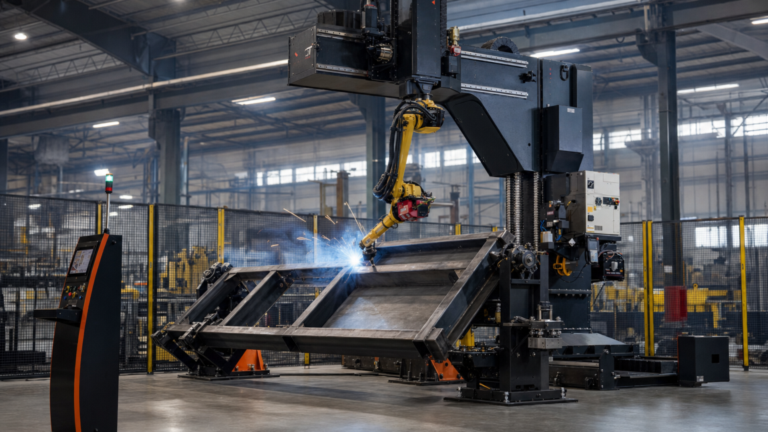
FANUC’s AI Welding Agent changes the software and upgrade questions around robotic welding, but it does not by itself remove the physical capacity, reach, positioning, workholding, and process-control reasons to evaluate an AGT BLOK system now.
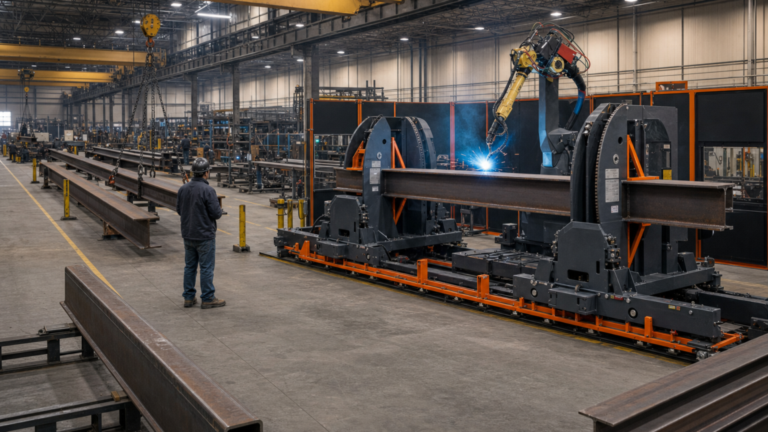
An AGT BeamMaster cell needs more than its published machine envelope. The Light, Plus, or Twin configuration must be matched to the longest member’s handling route, crane coverage, safeguarded access, fit-up, inspection, and outfeed staging.
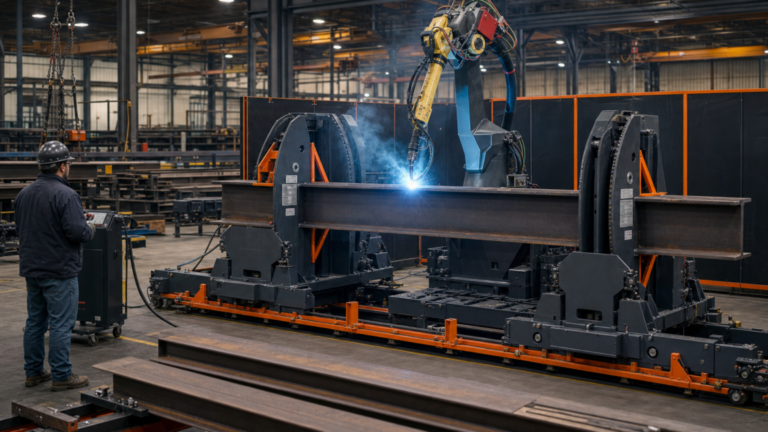
NovAI’s ABB and Yaskawa expansion changes the proof required in a robotic-welding capital review, but it does not justify delaying a needed structural-welding capacity investment.

The strongest first bridge welding automation scope is not necessarily the weld family with the most manual arc hours. It is the component that can move through engineering, fit-up, welding, inspection, repair, records, and outbound handling without an unresolved ownership or plant-flow gap.
End of content
End of content