Press Brake Control Retrofit Approval Starts With the Programming Handoff
The right control retrofit improves the path from programming through setup and first-part approval. The wrong scope simply moves delay from the brake to the office.

The right control retrofit improves the path from programming through setup and first-part approval. The wrong scope simply moves delay from the brake to the office.
Fiber laser automation improves press-brake flow only when cut blanks arrive separated, identified, staged, and matched to the intended brake program and tooling setup. Loading, unloading, storage, separation, and sorting solve different material-flow problems.

The Ermaksan Green Press FX Servo fits recurring bending work within its published 1.6 to 3.1 m and 40 to 100 ton range, but energy savings alone do not justify the investment. The stronger case comes from part fit, idle time, tooling, controls, quality risk, and lifecycle cost.
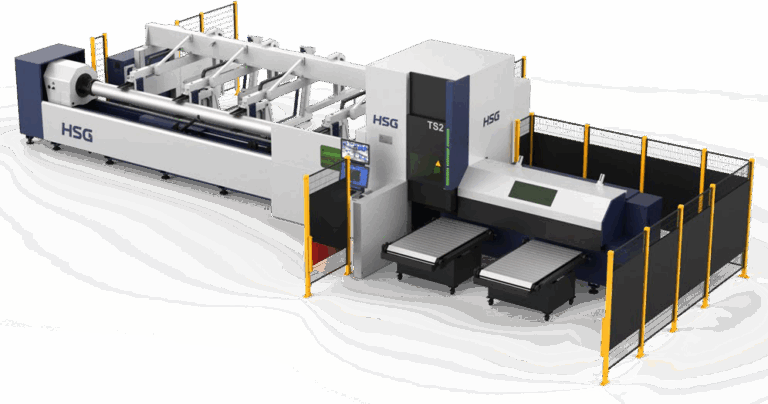
Checklist for evaluating an HSG tube laser upgrade for cut-to-bend: 3kW vs 6kW wattage, tube compensation, bending data handoff, OSHA-aligned guarding, and uptime prep.

Amada used laser + press brake retrofit checklist for Rockford, IL: verify laser interlocks/safety docs and confirm tooling fit + changeover readiness.
Used CNC Press Brakes: Controls Obsolescence + Guarding/LOTO Checks to protect uptime and ROI—pre-buy workflow for docs, spares, integration, and safety.
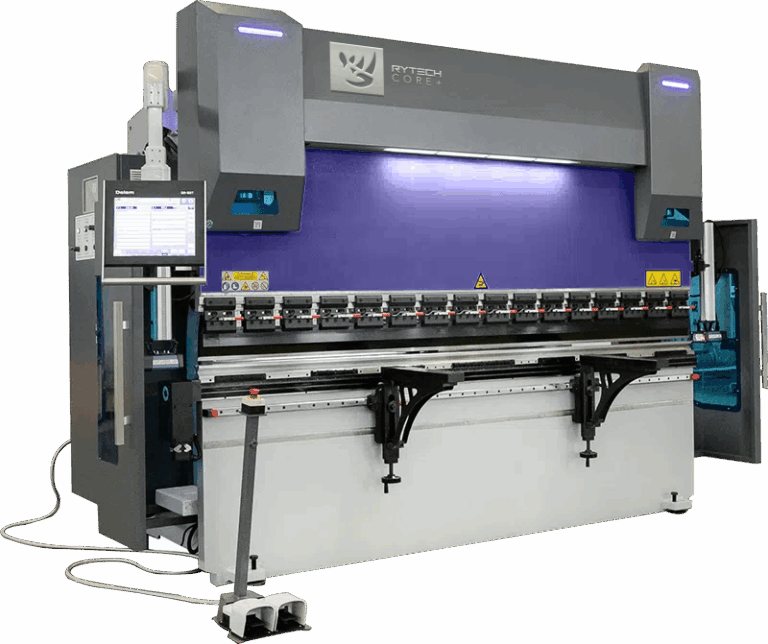
High-mix roofing, HVAC, and OEM bending often loses time at the press brake during changeovers. Explore a staged RYTECH CORE+ plan with OSHA-aligned safeguarding.
Evaluate Delem DA-Retrofit with Profile-T offline programming to cut press brake setup risk: connectivity checks, offline verification, adoption steps, and OSHA-ready safeguarding.
Use Delem (Profile-T) Offline Programming for Press Brakes to verify tooling feasibility, bend sequence, and collision risk—then plan a safe online handoff aligned to OSHA guarding.
End of content
End of content