PO (Purchase Order) to Production: How to Make Coil-Fed Roll Forming Lines Setup-Ready
Turn PO line items into machine-ready job data for coil-fed slit/CTL, coil handling, roll forming, and cut/folding—plus an OSHA-aligned SDS gate.


Turn PO line items into machine-ready job data for coil-fed slit/CTL, coil handling, roll forming, and cut/folding—plus an OSHA-aligned SDS gate.
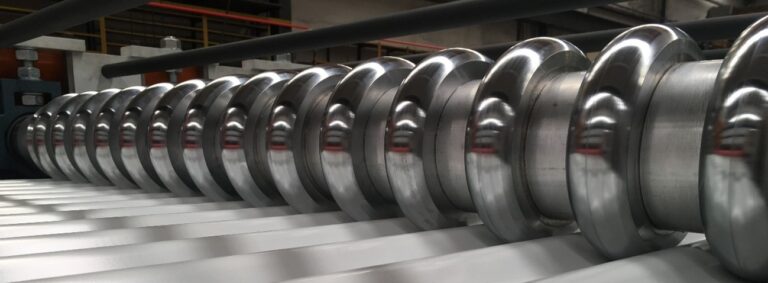
Stefa coil-fed roll forming setup reduction is workflow validation, not speed. Use this checklist to verify feed, cut/stamp, stacking, and OSHA guarding/LOTO.

When an automated station stops after hours, the fastest path back to production is clear data, trained people, and a support plan built before the alarm.
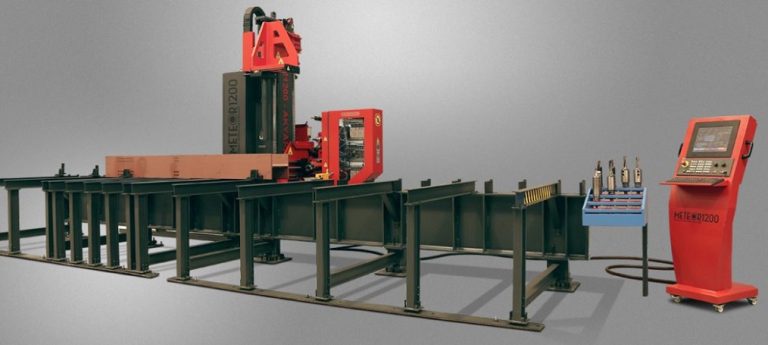
Use this shop-floor checklist for Akyapak BMB High Speed Flanging Machines to confirm automation-mode restart, OSHA 1910.212 guarding, and maintenance access.
Use this ACT cartridge pulse-cleaning buyer checklist: verify cleaning triggers and differential-pressure behavior, then align housekeeping with OSHA combustible-dust controls.
Turn your PO into machine-ready job data for Stefa coil-fed roll forming: standardize material/coating specs, slit/CTL intent, recipe fields, and the OSHA SDS gate.

Erbend’s Erfold Basic Line By Line as an ERFOLD Basic Line By Line setup reduction workflow: recipe repeatability, springback correction tests, and OSHA-guarded validation.
Press Brake Operator (PO) workflow creates setup time and first-part bend errors. Use OSHA guarding logic, consistent tooling, and staged flow to reduce rework.
Houston roofing and architectural sheet metal teams can judge when Stefa Coil-Fed Roll Forming Lines improve material flow, setup reduction, and staged upgrades more than speed.
End of content
End of content