Pat O’Neill
Pat O’Neill
Regional Sales Executive of Americas/National Product Manager
Born and raised in the southern suburbs of Chicago, graduated from Illinois State University where I also played rugby, moved to Milwaukee in 1991 and continued to play rugby for another 8 years. Married for over 30 years to my wife Lezli we have 2 sons and we love Wisconsin, Milwaukee and the Brewers.
related Articles
PMA’s September Survey and Coil-Line Capacity
PMA’s September survey shows cooler order expectations across a broad U.S. and Canadian metalforming sample, not a roofing or coil-line forecast. Coil-fed roll-forming buyers should weigh the signal against their own bookings, line use, profile mix, and production constraint.ERBEND MFE CNC Folder for Long Sheet Metal Parts
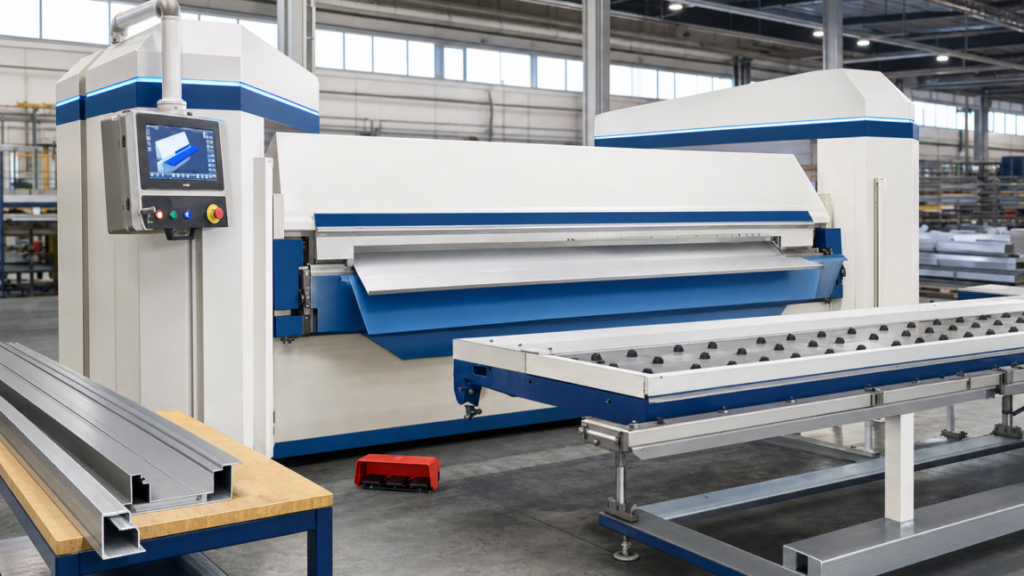
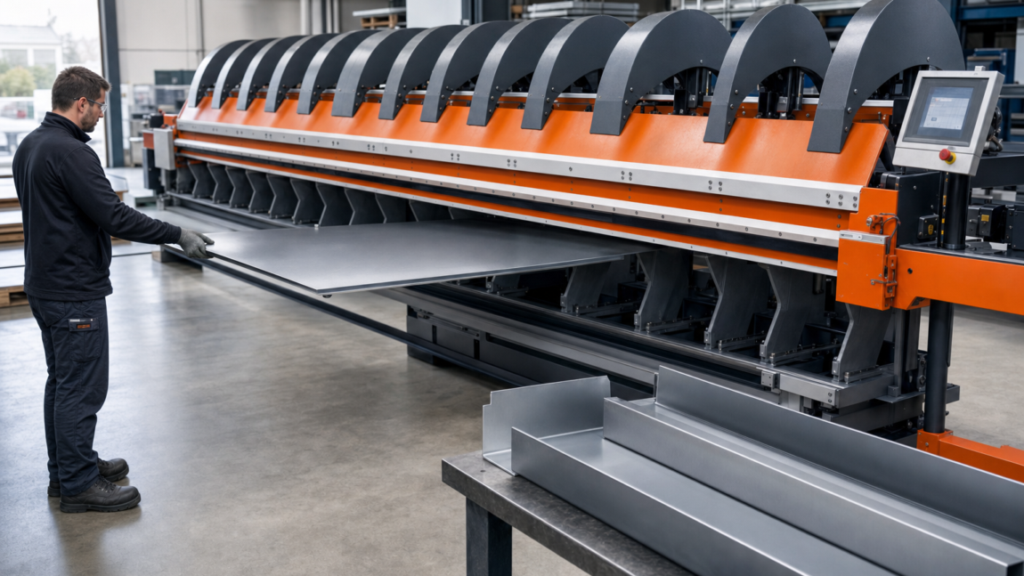
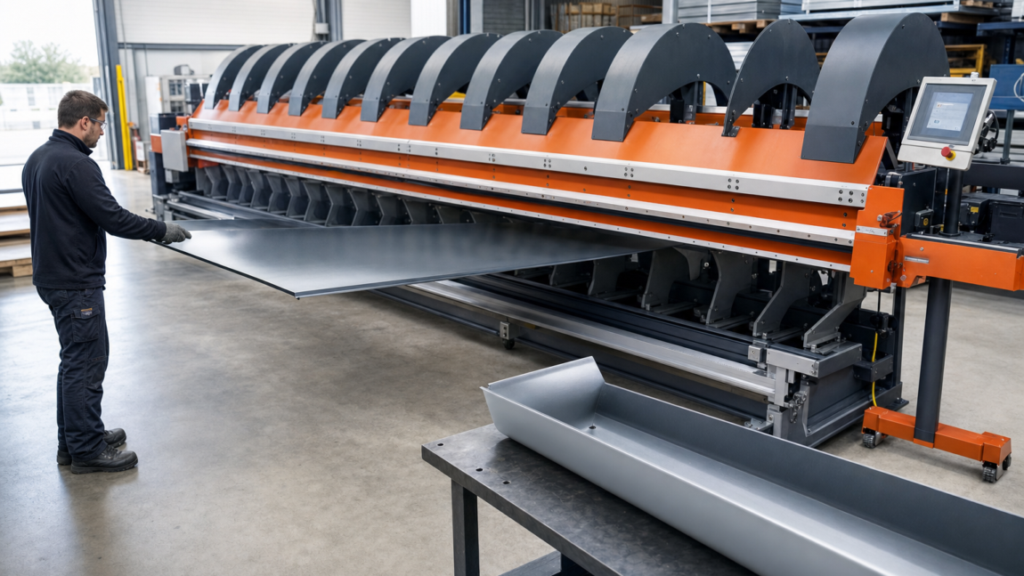
The ERBEND MFE METAL FOLDING MACHINE fits repeatable long-profile work when supported sheet handling, CNC positioning, and programmable folding matter more than press-brake tonnage or deep tooling access.STEFA VH315 for Thin-Sheet Cutting and Folding
The STEFA VH315 combines folder bending with a built-in shear and slitting function for suitable thin-sheet profiles. It fits variable roofing trim, flashings, rectangular profiles, narrow U-flanges, and custom architectural work when the material, blank, geometry, and feature requirements stay within the machine’s envelope.Hydraulic Plate Shear vs. Coil Processing
CMG’s new Omaha distribution facility makes sheet-to-part material flow worth revisiting, but the machine choice still depends on whether a shop needs batch blanking or continuous coil processing.Recoiler or Cut-to-Length Stacker?
Choose a recoiler when slit material must remain in coil form for shipment, storage, roll forming, or another coil-fed process. Choose cut-to-length stacking when the finished product must be a flat blank, then confirm the STEFA EH1000 configuration against the actual coil, strip, speed, handling, and downstream requirements.2026 Construction Rollforming Show: Fixed Roofing Roll-Forming Line Fit
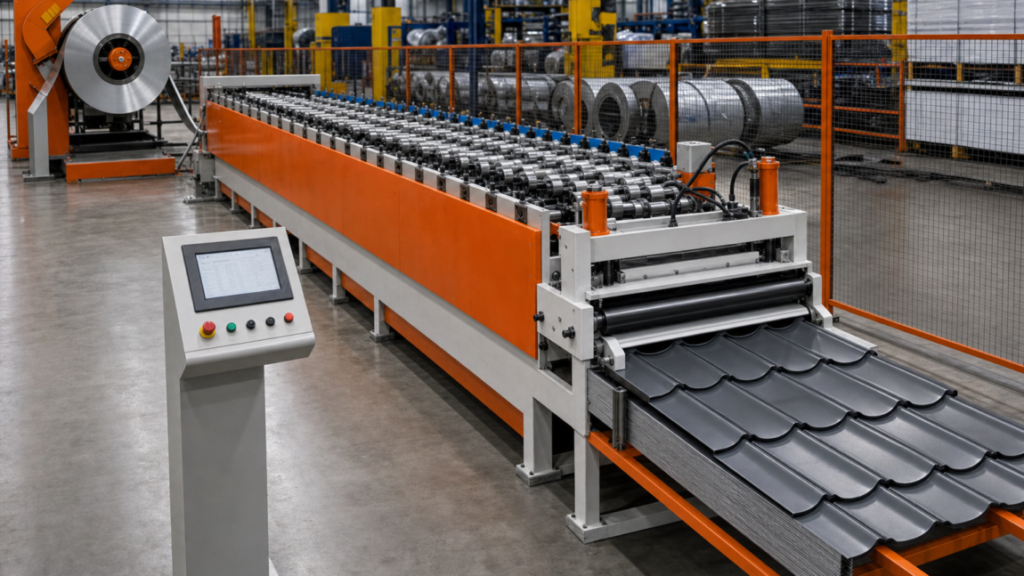
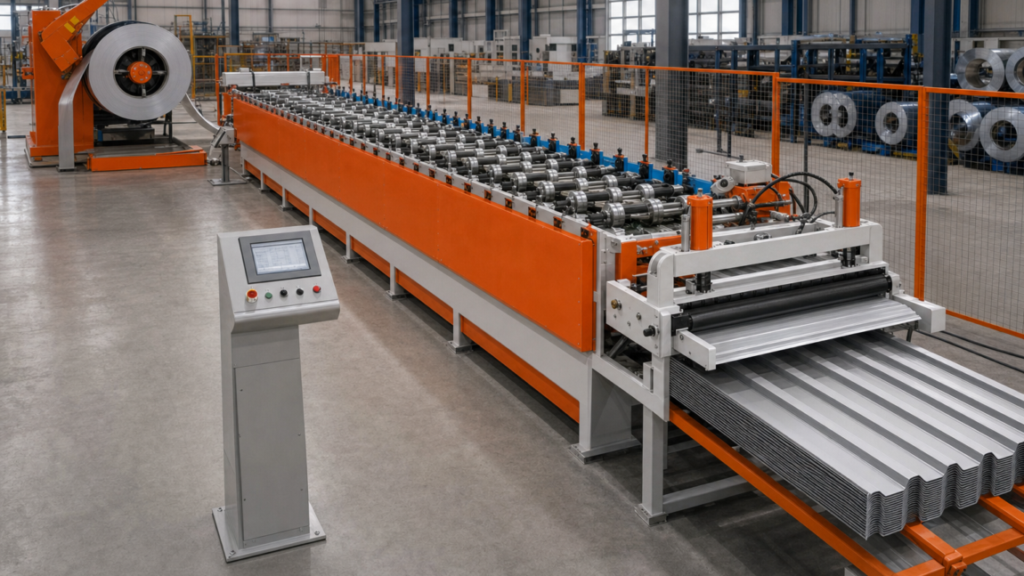
With the Construction Rollforming Show set for September 16–17, 2026, the STEFA ROLL FORMER LINE provides a concrete way to examine when fixed, multi-profile roofing production fits a plant—and what profile, coil, cutoff, handling, and site facts still need proof.Variable-Rake vs. Swing-Beam Shears for Plate Work
Choose a variable-rake guillotine shear for frequent changes in material and thickness; choose a swing-beam shear when repeat work fits a narrower capacity and adjustment range.LUXR Metal Shingles: Fixed Roll-Forming Line Fit
The June 25, 2026 LUXR announcement creates a reason to evaluate new roofing work, but it does not prove that a four-profile fixed line can produce the new shingle geometry. The STEFA ROLL FORMER LINE has to be qualified against the profile, coil, cutoff, changeover, discharge, packaging, and repeat-volume requirements.STEFA LCS3 for Coil Slitting and Cut-to-Length Blanking
The STEFA LCS3 combines coil straightening, longitudinal slitting, controlled feeding, and transverse shearing for fabricators that need repeatable strips and blanks from master coil. Its fit depends on material strength, coil dimensions, knife patterns, blank requirements, and downstream handling.Stefa VHB/VH or a Gutter Roll Former?
The Stefa VHB/VH long-folder family fits variable commercial-gutter and trim work, while a dedicated gutter roll former is better suited to high-volume repeat profiles made continuously from coil.Stefa Roll Former Line Automation: What It Controls
The Mac-Tech-listed Stefa Roll Former Line automates stored-job production, encoder positioning, loop control, profiled cutoff, and pneumatic unloading for four roofing profiles. Physical profile setup, material qualification, inspection, and safe maintenance still depend on the production team.Mac-Shear MRGM 3060-04 for Straight Sheet Cutting
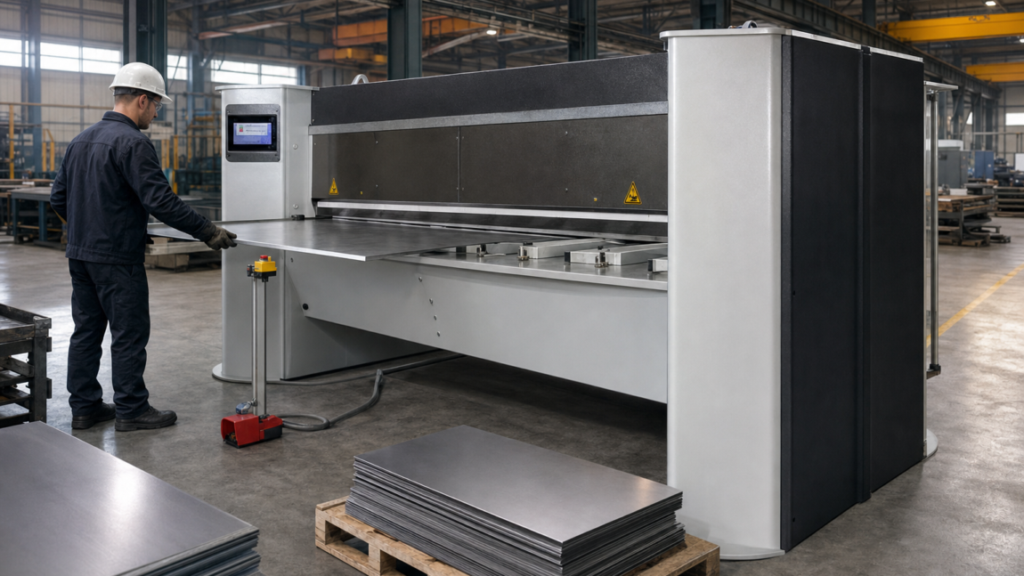
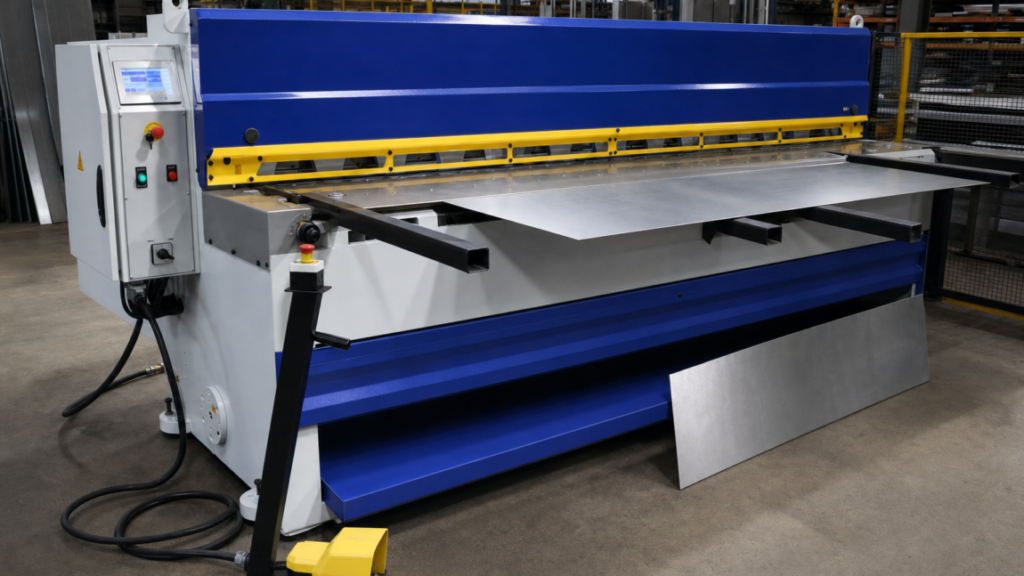
The Mac-Shear MRGM 3060-04 fits fabricators whose repeat work is mostly straight strips, rectangular blanks, and flat panels, provided the cut list stays within the machine’s listed 4 mm or 9-gauge steel rating and the 3060 mm or 10-foot model designation matches the actual sheet-handling plan. Its backgauge, squaring equipment, ball-transfer table, multi-edge blades, and optional controls support repeatable blank preparation, but geometry, alloy, handling, guarding, and downstream flow determine the final fit.